Ningbo Bolly biology Co., Ltd. is a leading China vegetal protein manufacturer specializing in high-quality plant protein ingredients for food and beverage applications. With a strong commitment to innovation, quality, and sustainability, the company provides comprehensive plant-based protein solutions to customers worldwide.
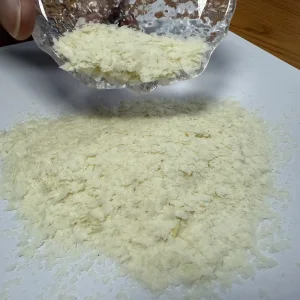
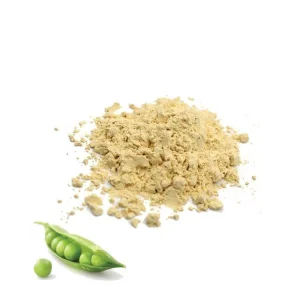
Leveraging advanced production technologies and strict quality management systems, Ningbo Bolly biology offers a diverse portfolio of vegetal protein ingredients, including soy protein, pea protein, rice protein, wheat protein, and other specialty plant proteins. These ingredients are widely used in functional foods, beverages, nutritional supplements, sports nutrition products, meat alternatives, dairy alternatives, bakery products, and health foods.
The company places great emphasis on research and development, continuously exploring new plant protein technologies to meet the evolving demands of the global food industry. Its experienced R&D team works closely with customers to develop customized ingredient solutions that enhance nutritional value, improve texture, optimize taste, and support clean-label product development.
Quality and safety are at the core of Ningbo Bolly biology' operations. The company implements rigorous quality control procedures throughout the entire production process, ensuring that all products meet international standards and customer requirements. By maintaining consistent product quality and reliable supply capabilities, the company has established long-term partnerships with food manufacturers, distributors, and brand owners across multiple international markets.
Driven by customer satisfaction and sustainable development, Ningbo Bolly biology Co., Ltd. continues to deliver innovative vegetal protein solutions that help customers create healthier, more sustainable, and market-competitive food and beverage products worldwide.
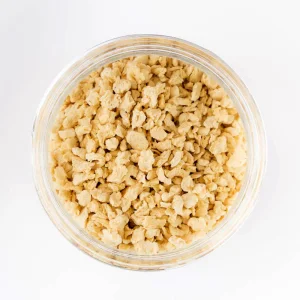
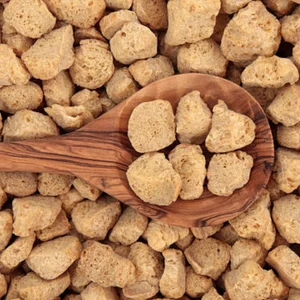
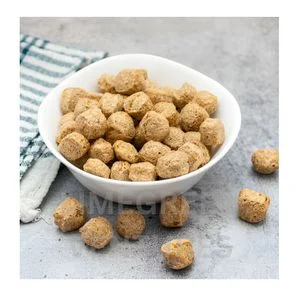
Modern consumers demand sustainable dietary alternatives without compromising on texture or protein bioavailability. Our textured vegetable proteins (TVP) and hydrolyzed peptides mimic animal muscle fiber structures with precision, ensuring excellent moisture retention and bite fidelity across industrial food processing lines.
Hydrolyzed plant proteins offer superior solubility and rapid amino acid absorption kinetics compared to native proteins. Designed for clear protein waters, RTD beverages, and post-workout recovery powders, our ingredients deliver high-purity protein solutions with neutral taste profiles.
Integrating non-GMO organic bean and seed flours into baked goods elevates nutritional matrices, boosting protein content and dietary fiber while maintaining structural integrity, crumb softness, and extended shelf life stability.
By deploying advanced targeted enzymatic cleavage techniques, our laboratories precisely control the molecular weight distribution of plant peptides. This breakthrough reduces allergenicity, eliminates bitter off-notes, and maximizes peptide absorption efficiency for clinical and high-performance nutritional applications.
Our commitment to green manufacturing encompasses zero-waste water recirculation systems and renewable energy integration. We continuously optimize our extraction processes to lower carbon footprints while producing premium organic ingredients that satisfy rigorous global environmental standards.
Navigating international food safety regulations requires meticulous documentation and transparent supply chains. Ningbo Bolly biology provides full compliance dossiers, supporting seamless market entry across North America, the European Union, Southeast Asia, and the Middle East.
ISO22000, HACCP, Halal, Kosher, and USDA Organic certified manufacturing facilities meeting uncompromising global standards.
Tailored granulation, agglomeration, and premix blending services designed to match your precise regional manufacturing specifications.
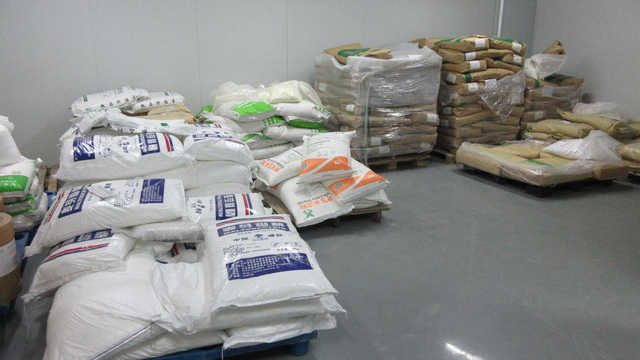
Strategic warehousing and robust global freight partnerships ensuring uninterrupted, on-time delivery for high-volume enterprise clients.
 Bolly Biology