Premium OEM/ODM raw materials, plant-based isolates, and bioactive peptides engineered for high functional efficacy.
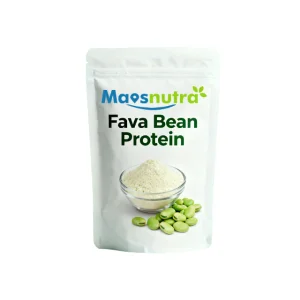
Analyzing the paradigm shift toward plant-dominant nutrition, bio-engineered peptides, and industrial-scale protein fortification.
The global high-protein ingredients market, valued at over USD 72.4 Billion in 2023, is projected to expand at a compound annual growth rate (CAGR) exceeding 7.8% through 2030. Escalating consumer demand for functional athletic supplements, clinical therapeutic diets, and plant-based meat analogues is accelerating bulk procurement demands worldwide.
Global regulatory bodies (FDA, EFSA, SAMR) and discerning retail consumers require clean-label ingredients. The industrial shift prioritizes hypoallergenic, non-GMO, organic certified isolates—such as hydrolyzed pea, chickpea, and rice proteins—replacing legacy synthetic fortifiers and high-allergen dairy derivatives.
Modern functional foods demand maximum biological availability. Bio-engineered oligopeptides extracted via targeted enzymatic hydrolysis demonstrate superior intestinal absorption rates, high thermal stability, and immediate cold-water solubility compared to native unhydrolyzed proteins.
| Protein Raw Source | Standard Protein Conc. (%) | PDCAAS Score | Solubility Profile | Key Target Applications |
|---|---|---|---|---|
| Soy Protein Isolate (SPI) | 85.0% - 90.0% | 1.00 | High Emulsification / High Water Retention | Meat Analogues (TVP), Nutritional Bars, Sports Shakes |
| Hydrolyzed Pea Protein | 80.0% - 85.0% | 0.89 - 0.93 | Instant Cold-Water Dispersible | Clean-Label Vegan Shakes, Medical Recovery Formulations |
| Organic Rice Protein | 80.0% - 85.0% | 0.85 | Suspension-Grade Fine Powder | Hypoallergenic Formulas, Infant & Elderly Nutrition |
| Chickpea Protein Isolate | 75.0% - 80.0% | 0.88 | Neutral Taste / Superior Gelling | Dairy-Free Cheese, Bakery Fortification, Gluten-Free Foods |
| Mung Bean Peptide | 80.0% - 88.0% | 0.91 | Ultra-Low Viscosity Bio-Peptide | Functional Energy Drinks, Anti-Fatigue Dietary Supplements |
Leveraging massive scale, fully automated bio-processing technology, and streamlined international logistics networks.
By controlling raw agricultural seed procurement directly from non-GMO farming clusters through to high-pressure extraction, ultrafiltration, and spray drying, Chinese factories dramatically reduce overhead costs while enforcing uniform raw material consistency.
Equipped with multi-stage membrane separation lines, continuous enzymatic reactors, and micro-encapsulation spray dryers, Chinese manufacturing hubs lead in creating debittered, highly soluble plant peptides engineered to client-specific molecular weight cutoffs.
With rapid pilot-scale testing lines, custom private-label packaging machinery, and direct deep-water port proximity (e.g., Ningbo Port), suppliers deliver ultra-competitive lead times and scalable Minimum Order Quantities (MOQs) tailored for multinational brands.
From functional consumer packaged goods to specialized industrial applications, high-protein extracts serve as vital active functional blocks.
High-protein formulas engineered for immediate Post-Workout Muscle Protein Synthesis (MPS). Incorporating custom blends of soy isolates, pea peptides, and oat beta-glucan into RTD (Ready-to-Drink) shakes, protein bars, and powdered meal replacements.
Textured Vegetable Protein (TVP) and high-solubility chickpea and fava bean isolates provide essential fibrous textures, bite density, and fat-emulsification properties required for realistic vegan burgers, sausages, and plant-based cheeses.
Specialized high-protein concentrates (e.g., Canola Meal, Meat and Bone Meal, high-protein rice protein) deliver concentrated amino acid profiles critical for accelerated growth, immune resilience, and feed conversion ratios (FCR) in poultry, cattle, and aquaculture.
Enzymatically hydrolyzed wheat proteins and botanical peptides penetrate hair shafts and dermal layers, acting as bio-moisturizers, protective film-formers, and structural repairing agents in premium shampoo, conditioners, and anti-aging creams.
Incorporating non-GMO whole grain durum flour, pumpkin seed protein powders, and mung bean extracts to boost protein density in gluten-free breads, keto cookies, extruded snacks, and high-protein pastas without compromising texture or mouthfeel.
Hypoallergenic, ultra-pure protein hydrolysates designed for rapid gastric emptying and seamless enteral tube administration, delivering vital nitrogen balances to geriatric, postoperative, or metabolic-compromised patients.
A transparent, standardized, and audit-ready manufacturing procedure designed for seamless integration into global supply chains.
Every batch of high-protein ingredient undergoes rigorous testing including High-Performance Liquid Chromatography (HPLC) for peptide distribution, Heavy Metal ICP-MS analysis, and Comprehensive Microbiological Screening prior to international dispatch.
Clients provide target nutritional specs, organoleptic criteria, solubility requirements, and sensory profiles. Our R&D lab formulates precise bench samples.
Execution of pilot production runs to issue full Certificate of Analysis (COA), allergen declarations, non-GMO verifications, and stability test reports.
Industrial automated processing, nitrogen-flushed bulk packaging (25kg bags, 50kg bags, or 1000kg super sacks) or retail-ready custom private label branding.
Full customs clearance documentation management including Phytosanitary Certificates, Health Certificates, Certificate of Origin, and container shipping.
Leading China Vegetal Protein Manufacturing Infrastructure & Biotechnology Operations
Ningbo Bolly biology Co., Ltd. is a leading China vegetal protein manufacturer specializing in high-quality plant protein ingredients for food and beverage applications. With a strong commitment to innovation, quality, and sustainability, the company provides comprehensive plant-based protein solutions to customers worldwide.
Leveraging advanced production technologies and strict quality management systems, Ningbo Bolly biology offers a diverse portfolio of vegetal protein ingredients, including soy protein, pea protein, rice protein, wheat protein, and other specialty plant proteins. These ingredients are widely used in functional foods, beverages, nutritional supplements, sports nutrition products, meat alternatives, dairy alternatives, bakery products, and health foods.
The company places great emphasis on research and development, continuously exploring new plant protein technologies to meet the evolving demands of the global food industry. Its experienced R&D team works closely with customers to develop customized ingredient solutions that enhance nutritional value, improve texture, optimize taste, and support clean-label product development.
Quality and safety are at the core of Ningbo Bolly biology' operations. The company implements rigorous quality control procedures throughout the entire production process, ensuring that all products meet international standards and customer requirements. By maintaining consistent product quality and reliable supply capabilities, the company has established long-term partnerships with food manufacturers, distributors, and brand owners across multiple international markets.
Driven by customer satisfaction and sustainable development, Ningbo Bolly biology Co., Ltd. continues to deliver innovative vegetal protein solutions that help customers create healthier, more sustainable, and market-competitive food and beverage products worldwide.
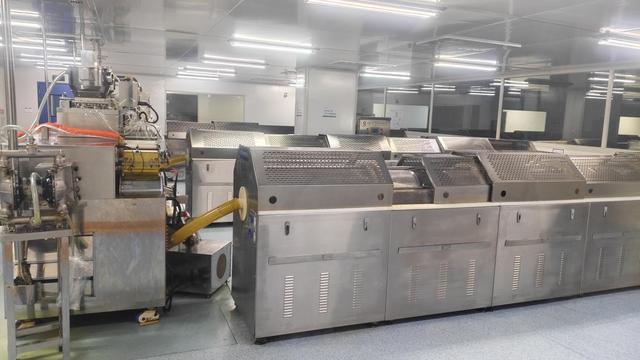
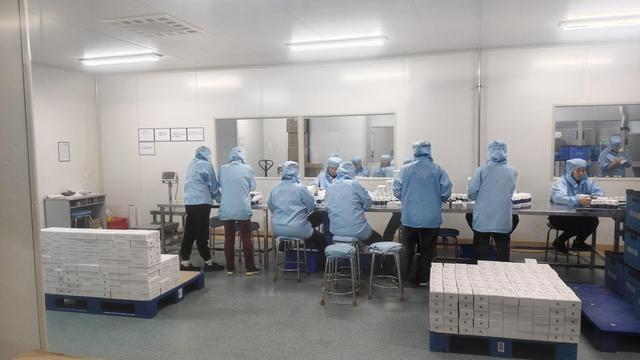
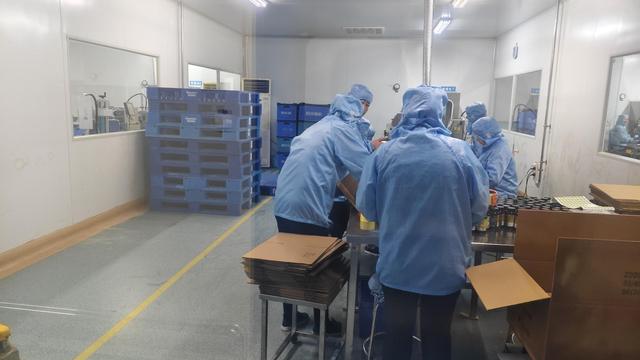
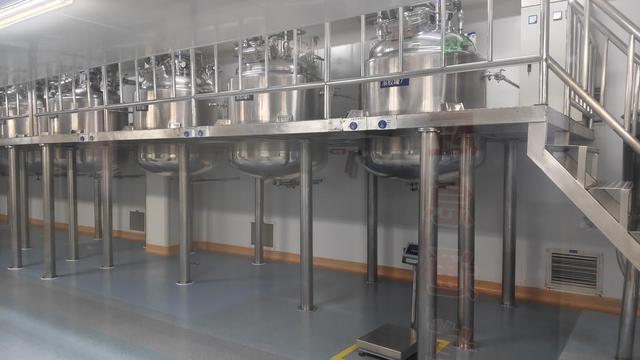
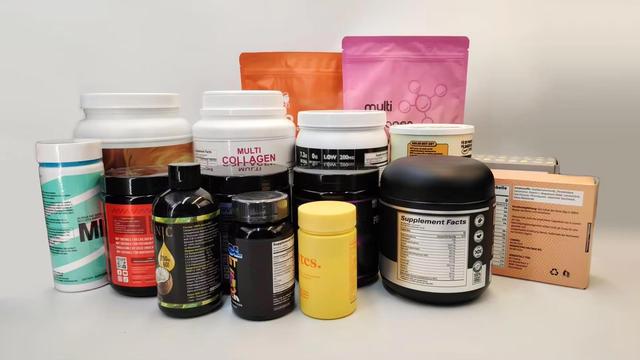
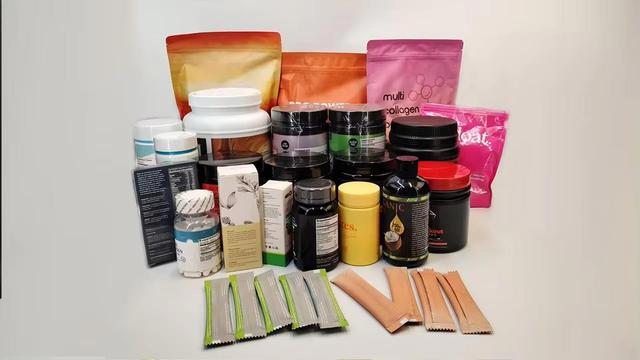
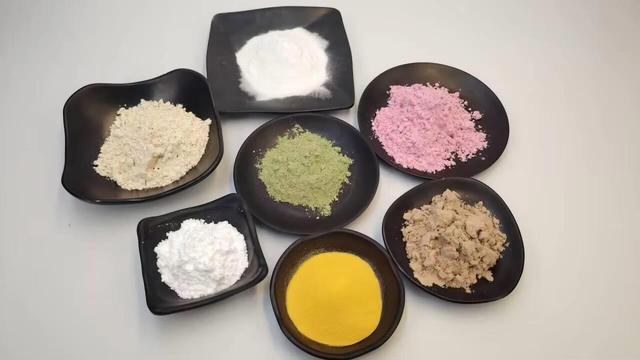
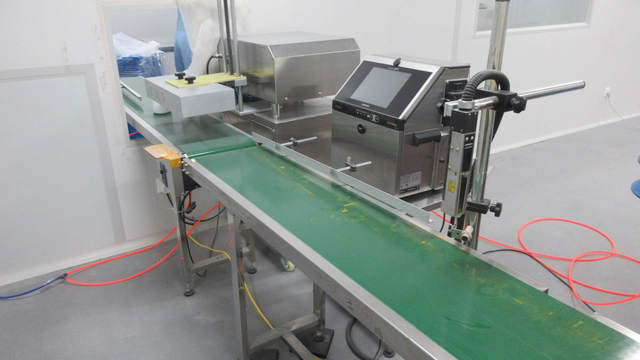
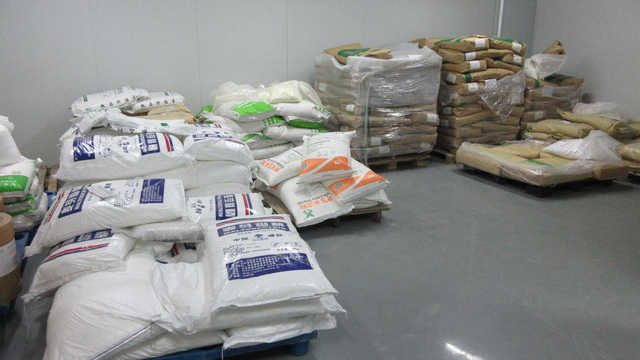
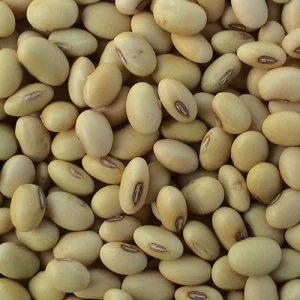
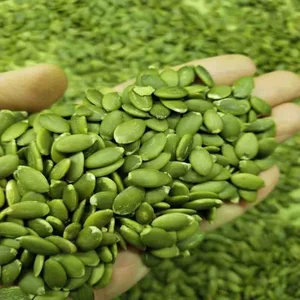
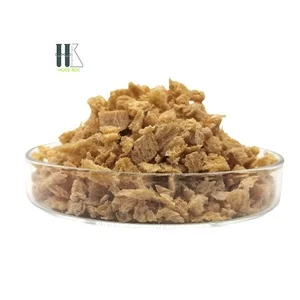
Comprehensive portfolio of botanical proteins, micro-algae extracts, feed grades, and textured functional ingredients.

Expert answers addressing quality control, MOQs, OEM capabilities, international regulatory compliance, and formulation science.
 Bolly Biology